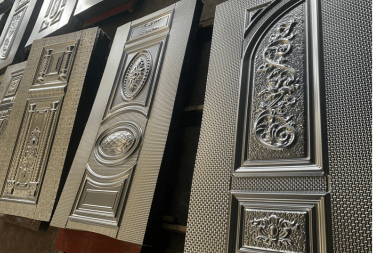
- 3000+ Patterns Are Available
- 008617749755602
- yoyicassia@hotmail.com
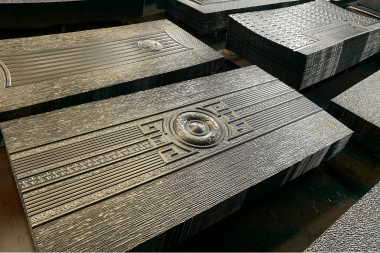
Steel Embossed Door Skin Sheet Manufacturing Process: A Complete Guide
The steel embossed door skin sheet manufacturing process is the backbone of modern steel entry door production. It converts raw cold rolled steel door skin coils into beautiful, durable, and weather‑resistant panels. Whether you need a wood grain transfer printing for steel doors or a simple geometric texture, understanding this door panel embossing process helps manufacturers optimize quality and reduce waste.
In this guide, we explain how steel embossed door skins are made—from decoiling to final powder coating—while highlighting the key equipment and quality checkpoints.
What Is an Embossed Steel Sheet for Doors?
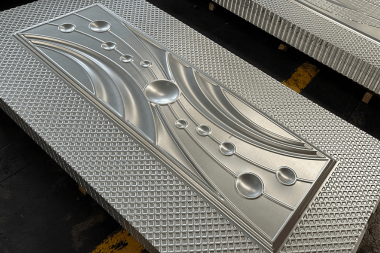
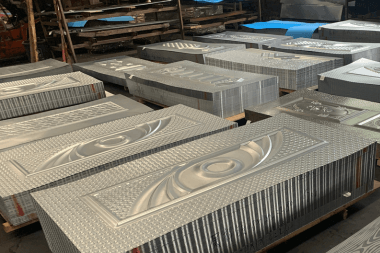
An embossed steel sheet for doors is a flat steel panel that has been pressed with a decorative pattern (wood grain, leather, vertical flutes, etc.) using a hydraulic embossing press. The raised or recessed texture hides minor surface flaws, increases rigidity, and provides an attractive finish. These sheets are typically made from cold rolled steel door skin coated with zinc (galvanized) to prevent rust.
Key Materials Used
Cold-rolled steel (SPCC, SGCC) – Thickness: 0.4 mm to 1.5mm
Galvanized or zinc-alloy coated steel – For corrosion resistance
Pre-painted color steel – Optional for direct finishing
Step‑by‑Step Manufacturing Process
1. Decoiling & Leveling (Raw Material Preparation)
The steel door skin production line starts with large coils of cold‑rolled or galvanized steel (thickness: 0.4 mm–2.0 mm). A decoiler unwinds the coil, and a leveling machine flattens the strip to remove any curvature. This ensures the embossed steel sheet for doors has a uniform thickness before further processing.
2. Cutting to Blank Size
The leveled strip is sheared into rectangular blanks using high‑speed automatic shears. Dimensional tolerances are kept within ±0.5 mm. Accurate blank sizing is critical for the subsequent door panel embossing process.
3. Door Skin Mold Design & Fabrication
Before embossing can begin, the embossing mold (also known as a door skin press die) must be designed and fabricated. The mold is a specialized tool used to create patterns, shapes, or textures on steel door surfaces. These molds are typically made of 45# steel and feature designs engraved or etched into the mold surface to create a raised or recessed pattern when pressed onto the steel material.
Mold designs range from simple geometric patterns to intricate motifs, wood grain textureshttps://www.yoyimachinery.com/products/door-embossing-mold/, and custom designs based on customer preferences. The mold core typically measures around 1600×520×31 mm for main doors and 1600×210×31 mm for sub-doors, with pattern design sizes generally around 1600×520 mm and 1600×210 mm respectively. This design phase often utilizes CAD software to ensure precision and visual appeal.
4. Embossing – Core of the Steel Embossed Door Skin Process
A. Hydraulic Press Embossing (Stamping Method)
The steel blank is placed between a male and a female die inside a hydraulic embossing press (2000–8000 tons capacity). The press applies high pressure, permanently deforming the steel to replicate the mold pattern. This is the heart of how steel embossed door skins are made.
Embossing depth usually ranges from 5mm to 30 mm, depending on sheet thickness and pattern complexity. For high volume production, manufacturers use a steel door skin embossing machine with automatic feeding and ejection systems. An alternative method is roller embossing, but hydraulic pressing offers superior depth and detail.
B. Roller Embossing Method
As an alternative to hydraulic stamping, some manufacturers use roller embossing machines, which utilize rotating embossing rollers to press patterns into steel sheets through continuous rolling action. This method is more cost-effective for large-volume manufacturing and supports both single-side and double-sided configurations, but it is generally limited to repetitive, linear patterns and offers less depth and detail compared to hydraulic methods.
5. Shearing to Final Door Dimensions
After embossing, the embossed steel sheets proceed to shearing—cutting the sheets to the precise dimensions required for the door panels. Precision shearing ensures the edges are perfectly square, preparing the sheet for later bending and folding.
6. Punching – Holes for Hardware
A CNC punch press (25–35 ton) creates all necessary openings in one or multiple strokes:
Handle and lock holes
Hinge recesses
Peephole and doorbell cutouts
Side lock slots
CNC positioning guarantees that every hole aligns exactly with standard hardware templates. This step is essential for a seamless final assembly.
7. Bending & Forming the Door Skin
Using CNC press brakes, the flat embossed sheet is bent along the edges to form a shallow pan shape (the door skin). This creates the return flanges that will later be folded over the core material and back panel. Accurate bending prevents warping and ensures a tight fit with the door frame.
8. Welding Reinforcements
Small internal brackets, lock reinforcements, and hinge stiffeners are spot‑welded or MIG‑welded to the inside of the door skin. All welds are ground smooth to avoid interfering with the core material. This step adds structural strength to the final door.
9. Surface Pretreatment (Phosphating)
Before coating, the steel skin goes through a multi‑stage chemical bath:
Degreasing – removes oils and dirt
Pickling – removes rust and mill scale
Phosphating – applies a zinc or iron phosphate conversion coating
This phosphate layer dramatically improves paint adhesion and corrosion resistance, which is vital for long‑lasting powder coated steel door skin products.
10. Coating & Wood Grain Transfer Printing
For solid colors: Electrostatic powder coating (polyester or epoxy‑polyester) is applied, then cured in an oven at ~200 °C (392 °F). The result is a durable, chip‑resistant powder coated steel door skin.
For wood grain finishes: A wood grain transfer printing for steel doors process is used. A transfer film bearing the wood pattern is heat‑pressed onto a pre‑coated base layer. This gives the steel the realistic look of oak, cherry, or mahogany while retaining all the benefits of steel.
11. Core Filling & Lamination (For Insulated Doors)
If the door is intended as an insulated entry door, the hollow cavity between front and back skins is filled with:
Polyurethane foam – injected as liquid, expands to fill every void
Honeycomb paper – for lightweight, non‑insulated applications
The front and back steel embossed door skin panels are then bonded together using a hydraulic hot press laminating machine. Heat and pressure create a permanent, warp‑free sandwich structure.
12. Edge Folding (Seaming)
The edges of the front and back panels are mechanically folded over each other using a specialized edge‑folding machine. This produces a tight, seamless joint that prevents moisture ingress and adds structural rigidity. Proper edge folding is a hallmark of a high‑quality steel door skin production line.
13. Final Assembly & Hardware Installation
Weatherstripping (EPDM or silicone) is inserted into the perimeter channel. Locks, handles, hinges, and peepholes are mounted using the pre‑punched holes. Each door is tested for smooth operation and proper sealing.
Quality Control in Door Skin Production
Strict quality control in door skin production is maintained at every stage:
| Stage | Inspection Checkpoint |
|---|---|
| Incoming steel | Thickness, coating uniformity, surface defects |
| After embossing | Embossing depth and pattern clarity (no tearing) |
| After punching | Hole positions, burr height |
| After welding | Weld strength, spatter removal |
| After pretreatment | Phosphate crystal size, coverage |
| After coating | Gloss level, hardness, cross‑hatch adhesion |
| Final assembly | Lock function, hinge alignment, weather seal |
Modern lines use automated vision systems to measure embossing depth and pattern clarity in real time, ensuring every panel meets specifications.
Equipment in an Automated Steel Door Manufacturing Line
Decoiler & leveling machine
CNC laser cutting machine
Hydraulic embossing press (2000T – 8000T) Steel door skin embossing machine
CNC turret punch press
CNC press brake
Spot welder / MIG welder
Multi‑stage phosphating tunnel
Electrostatic powder coating booth & curing oven
Wood grain transfer printing for steel doors machine
Foam injection machine
Hot press laminator
Edge folding machine
An automated steel door manufacturing line can produce 200–800 doors per shift with minimal manual intervention.
Frequently Asked Questions (FAQ)
1. What thickness of cold rolled steel door skin is best?
20‑gauge (0.9 mm) and 24‑gauge (0.6 mm) are most common. Thicker steel offers better security but adds weight.
2. Can embossed steel sheet for doors be painted after installation?
Yes, but factory powder coated steel door skin is far more durable. Field painting requires proper cleaning and etching primer.
3. How long does a door skin mold last?
A hardened steel mold can produce 100,000–500,000 door skins before needing refurbishment.
4. What is the difference between embossed and plain steel door skins?
Embossed skins have a decorative texture; plain skins are smooth and require a separate finish. The door panel embossing process adds both beauty and rigidity.
5. Can I get a wood grain finish on steel?
Yes – wood grain transfer printing for steel doors creates a realistic wood appearance that never rots, cracks, or fades like real wood.
Conclusion
The steel embossed door skin sheet manufacturing process is a sophisticated blend of heavy stamping, precision cutting, advanced coating, and strict quality control in door skin production. By understanding how steel embossed door skins are made, manufacturers can optimize their steel door skin production line to produce beautiful, secure, and long‑lasting entry doors.
For companies looking to invest in a new hydraulic embossing press or upgrade their door skin mold design, partnering with experienced machinery suppliers is the key to achieving consistent embossing depth and pattern clarity at high volume.